1. Strategic Market Context & International Regulatory Architecture
The global absorbent hygiene industry is undergoing an unprecedented structural transformation driven by irreversible demographic aging across developed and middle-income nations. By 2026, the global population aged 65 and older exceeds 800 million individuals. In super-aged societies such as Japan, Germany, Italy, and South Korea, gross retail and institutional expenditures on adult incontinence products have officially outpaced infant diaper volumes. For international healthcare distributors, public hospital procurement agencies, and private-label retail conglomerates, this shift elevates adult incontinence from a secondary niche into the primary volume and margin driver of the global nonwovens sector.
Historically, commercial adult diaper purchasing was treated as a transactional commodity trade governed strictly by low cost-per-unit metrics. However, modern healthcare economics have fundamentally rewritten institutional procurement criteria. In professional nursing homes and hospital geriatric wards throughout Western Europe, North America, and Latin America, clinical directors evaluate the total cost of care. Low-grade adult briefs characterized by high rewet values, poor breathability, and unstable core integrity inevitably cause severe secondary complications, most notably Incontinence-Associated Dermatitis (IAD) and Stage I-IV pressure ulcers. Treating an advanced pressure injury can cost hospital networks upwards of $10,000 in specialized clinical labor, sterile dressings, and prolonged bed stays. Consequently, national healthcare tenders increasingly mandate compliance with ISO 11948-1 (Rothwell Method) (Rothwell Method) total absorbency minimums and verified low rewet thresholds.
Simultaneously, regulatory oversight for adult medical incontinence has tightened globally. In the United States, adult briefs and bed underpads fall under U.S. FDA 21 CFR 880.5270 as Class I medical devices requiring foreign establishment registration and active device listings. In the European Union, the Medical Device Regulation (European CE MDR (EU 2017/745)) imposes strict post-market surveillance, biocompatibility validation under ISO 10993, and technical documentation auditing. Operating from Quanzhou, China since 2004, Quanzhou Shenghongda Hygiene Products Co., Ltd. provides international B2B partners with an unassailable compliance foundation across 16 full-servo high-speed converting lines, producing over 1.2 billion units annually across OEM Adult Diapers with Tapes, Adult Incontinence Pull-Up Pants, Disposable Hospital Bed Underpads, and Anatomical Booster Incontinence Pads.
By maintaining accredited in-house testing under CNAS National Accreditation guidelines and holding 12 global certifications, Shenghongda ensures that international importers, private label brand owners, and healthcare distributors minimize customs clearance risks, protect brand integrity, and achieve optimal landed procurement costs across more than 88 export destination nations.
2. Raw Material Chemistry, Polymer Kinetics & Core Architecture
Engineered for maximum overnight retention, modern adult briefs require an intricate balance of polymer chemistry, fiber capillarity, and fluid-dynamics engineering. Adult incontinence briefs operate under severe hydrostatic pressures. When a recumbent patient shifts bodyweight, mechanical pressure exceeding 0.5 psi (3.5 kPa) is exerted directly upon the wetted absorbent core. If the internal superabsorbent polymer (SAP) matrix suffers from gel blocking or insufficient cross-linking density, trapped urine is forced back against fragile perineal skin, causing rapid maceration and precipitating IAD. Shenghongda’s dual-core architecture incorporates Japanese Sumitomo Seika Chemicals (Japan) Aqua Keep SA60 polymers with high Absorbency Under Load (AUL ≥ 24 g/g at 0.7 psi) and untreated virgin softwood kraft fluff pulp from Weyerhaeuser Company (USA), preventing core collapse and maintaining an ultra-low surface rewet profile below 0.05 grams.
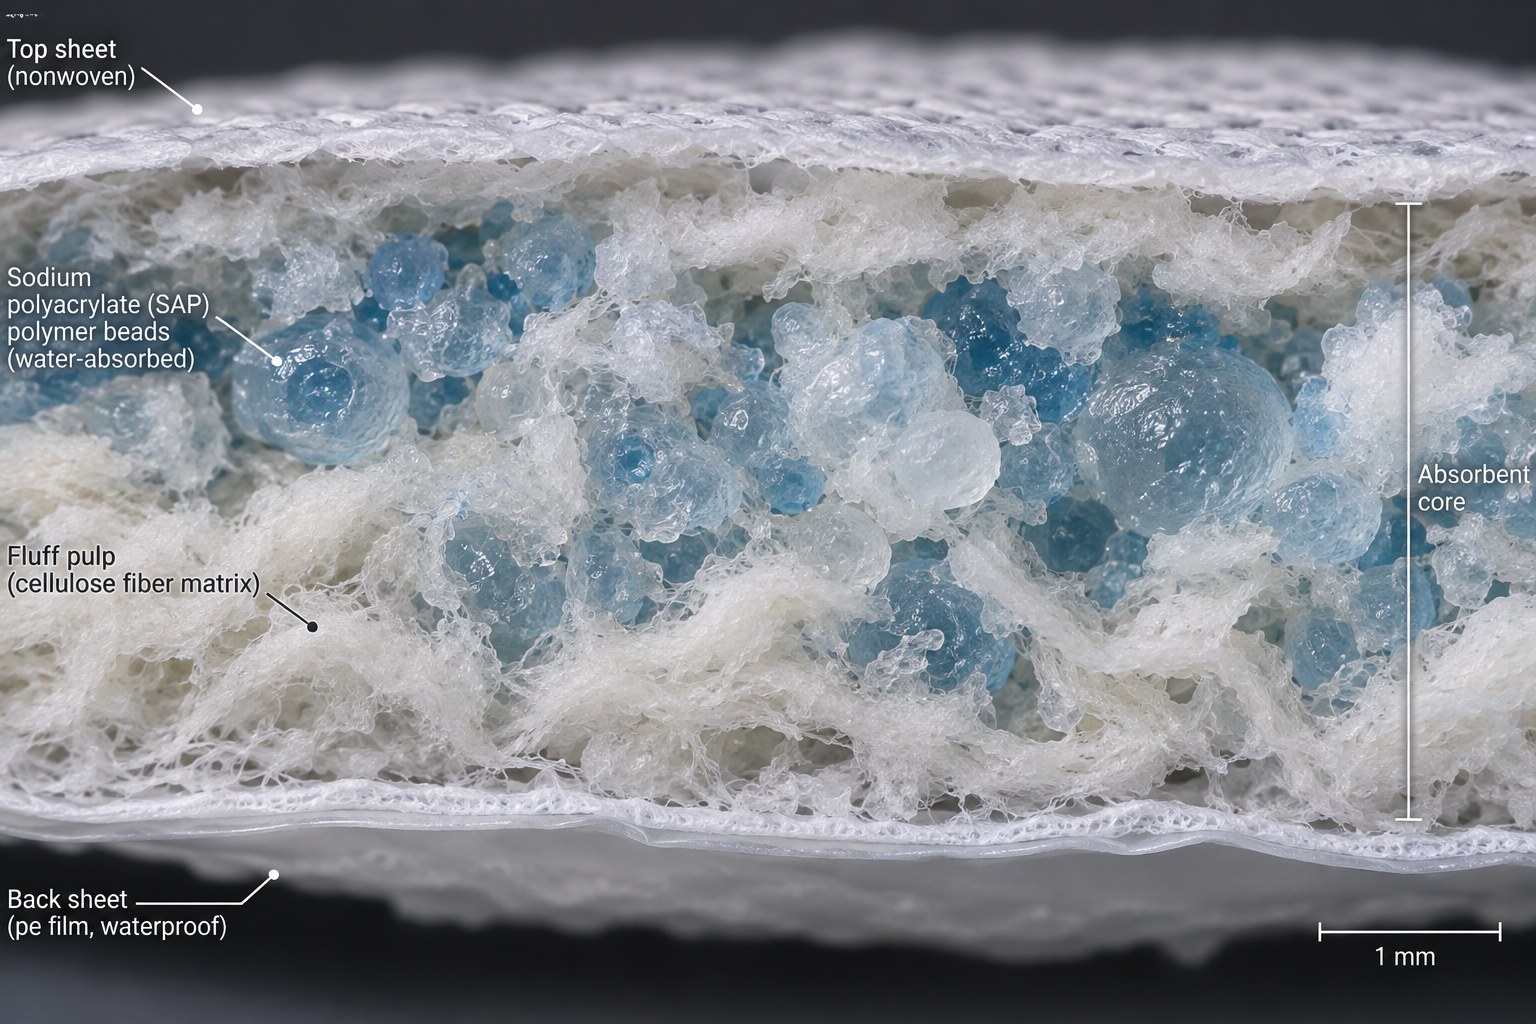
The primary functional engine is cross-linked sodium polyacrylate ($[-CH_2-CH(COONa)-]_n$) featuring precise surface cross-linking gradients and particle size distributions strictly calibrated between 150 and 850 microns. This morphology delivers a Centrifugal Retention Capacity (CRC) of ≥32 g/g and Absorbency Under Load (AUL at 0.7 psi / 4.8 kPa) of ≥24 g/g. Under severe patient compression, these polymer beads maintain structural rigidity, continuing to draw fluid away from the skin surface through sustained osmotic swelling pressure.
Complementing the synthetic polymer granules is virgin Southern Bleached Softwood Kraft (SBSK) fluff pulp, sourced directly from certified American producer Weyerhaeuser Company (USA) (Golden Isles brand). Virgin softwood pulp fibers exhibit an average length of 2.6 to 2.8 millimeters, providing a natural 3D open-pore capillary network that rapidly diffuses liquid insults along the longitudinal core axis before SAP granules reach maximum swelling equilibrium. Inline hammermills with automated fiber-fractionation air-laid drums ensure a uniform core density of 0.12 to 0.14 g/cm³, preventing localized clumping or core cracking during active movement.
Surrounding the internal absorbent core is an engineered fluid-management envelope comprising a high-loft Acquisition Distribution Layer (ADL) of through-air bonded nonwoven (35-50 g/m²) and an ultra-soft hydrophilic topsheet. When high-velocity urinary surges occur—often exceeding 60 to 80 ml in fewer than 3 seconds—the topsheet instantly transmits the liquid downward without pooling. On the exterior barrier, Shenghongda applies breathable microporous polyethylene films laminated with spunbond nonwovens, achieving a Moisture Vapor Transmission Rate (MVTR) exceeding 3,500 g/m²/24h. This microclimate engineering enables warm, humid air molecules to escape continuously while retaining absolute liquid impermeability, dramatically reducing skin maceration risks.
| Functional Layer / Raw Material | Chemical & Physical Specification | Primary Global Supplier | Key Performance Metric | Verification Standard |
|---|---|---|---|---|
| Dual-Core Superabsorbent Polymer (SAP) | Sumitomo Seika Aqua Keep SA60 (Japan) | Sumitomo Seika / Sanyo San-Dia | CRC ≥ 32 g/g; AUL (0.7 psi) ≥ 24 g/g | EDANA NWSP 241.0 / 242.0 |
| Virgin Softwood Fluff Pulp | Weyerhaeuser Golden Isles SBSK (USA) | Weyerhaeuser / Stora Enso | Fiber length 2.6 mm, Moisture ≤ 8.0% | ISO 5351 / FSC-STD-40-004 |
| Acquisition Distribution Layer (ADL) | Through-air bonded nonwoven (PET/PE bicomponent) | Tier-1 Nonwoven Mills | Basis weight 45 g/m², Strike-through < 1.8s | EDANA NWSP 070.1.R2 |
| Hydrophobic Standing Leak Barriers | Spunbond-Meltblown-Spunbond (SMS) nonwoven | Toray / Fibertex | Hydrostatic head > 220 mm H₂O, 4 Lycra strands | ISO 1420 / EDANA NWSP 120.1 |
| Breathable Microporous Backsheet | Breathable PE film laminated with spunbond PP | Formosa Plastics / In-House | MVTR ≥ 3,500 g/m²/24h, Zero pinhole leakage | ASTM E96 / JIS Z 0208 |
| Fastening Closure System | Multi-refastenable polypropylene hook & loop tabs | 3M / Aplix | Peel strength > 3.8 N/25mm, Shear > 15 N | ASTM D1876 / Tensile Tester |
3. Production Automation, High-Speed Converting Lines & Defect Control
The transition from polymer chemistry to mass-produced adult incontinence articles requires state-of-the-art converting automation. High-speed manufacturing of adult briefs involves synchronizing up to fourteen discrete continuous material webs—including nonwoven topsheets, tissue carriers, pulp ribbons, superabsorbent powder streams, elastic spandex threads, frontal tapes, side release tabs, and polyethylene backing films—moving at linear velocities exceeding 350 to 500 meters per minute. A mechanical variance of a single millimeter or a microscopic tension fluctuation can result in web breakage, defective product geometry, or catastrophic adhesive misplacement. To guarantee absolute batch consistency across annual export volumes surpassing 1.2 billion pieces, Shenghongda operates Japanese Zuiko Corporation and European Fameccanica full-servo automated converting machinery.
Unlike legacy semi-servo or mechanical line-shaft drive systems that rely on complex gearboxes, timing belts, and line shafts susceptible to mechanical backlash, thermal expansion, and progressive mechanical wear, Shenghongda’s converting lines utilize independent digital servo motors directly coupled to each critical process module. Every unwinding stand, rotary cutting die, embossing drum, and vacuum transfer belt is controlled by centralized high-speed Programmable Logic Controllers (PLCs) running real-time industrial Ethernet protocols. This allows our mechanical engineers to fine-tune web tensions dynamically down to 0.1 Newton-meters across varying environmental ambient temperatures and humidity levels. Furthermore, our raw material unwinding stands feature automated zero-speed butt splicers, allowing 1,500-meter parent rolls of nonwoven fabric and virgin fluff pulp to be seamlessly spliced on the fly at full operating speed, entirely eliminating the production downtime and thermal glue degradation associated with manual roll changeovers.
Quality assurance on high-speed converting lines demands continuous, 100% inline automated surveillance. Shenghongda’s lines are equipped with multi-camera high-resolution CCD machine vision inspection systems positioned at critical assembly stages. Operating under pulsed high-intensity LED strobe illumination, these computerized vision cameras capture micro-second images of every single diaper unit traveling down the conveyor belt. Dedicated optical algorithms analyze each product in real-time, instantly identifying and flagging micro-defects including:
- Absorbent Core Alignment: Verifying longitudinal and lateral placement of the fluff-SAP pad within a tolerance of ±1.5 mm relative to the chassis edge.
- Foreign Particulate Contamination: Detecting minute foreign fibers, dark specks, or insect contamination down to 0.3 mm² surface area.
- Adhesive Bleed-Through and Misplacement: Identifying excess hot-melt adhesive or insufficient glue spray width on standing leg cuffs.
- Elastic Strand Tension & Count: Confirming all four Lycra elastic strands in the 3D standing leak barriers are intact and under equal elongation tension.
- Side Tape & Landing Zone Placement: Inspecting mechanical hook tape symmetry to prevent unfastenable closures during bedside clinical application.
4. Empirical Laboratory Testing & CNAS-Standard Clinical Validation
To substantiate all marketing claims and satisfy the rigorous regulatory scrutiny of international medical device agencies, every production lot manufactured at Shenghongda undergoes extensive physical, chemical, and microbiological testing in our dedicated, in-house testing facility operated strictly in accordance with CNAS National Accreditation and ISO 9001:2015 quality management protocols. Our laboratory testing matrix covers both dynamic fluid-handling behavior and physical mechanical durability, ensuring that our products perform flawlessly under severe clinical nursing conditions.
The primary global gold standard for assessing adult incontinence capacity is the ISO 11948-1 (Rothwell Method) Rothwell Method. In this test protocol, full diaper samples are weighed dry, completely submerged in a 0.9% sodium chloride saline bath for precisely 30 minutes to achieve absolute liquid saturation, removed and suspended vertically for 30 seconds to allow excess surface moisture to drain freely, and then re-weighed on high-precision analytical balances. The difference between the saturated wet mass and the dry mass defines the Total Absorbency Capacity (TAC). While many commercial manufacturers quote inflated, theoretical free-swell absorption values, Shenghongda strictly reports verified Rothwell retention figures—ranging from 1,800 ml for daytime active briefs up to 3,500 ml for maximum-overnight clinical tenders—providing hospital procurement committees with an unassailable engineering fact base.
Equally critical is the Surface Rewet Under Load test, evaluated under EDANA Standards NWSP 070.1.R2 protocols. A product may possess high gross fluid capacity, but if that absorbed fluid readily migrates back to the surface when a bedridden patient shifts weight, the surrounding stratum corneum will become severely macerated, precipitating rapid skin breakdown. In our testing regime, following three consecutive 100 ml saline insults delivered at calibrated 20-minute intervals, a standardized stack of pre-weighed laboratory filter paper is placed over the insult zone, and a mechanical dead-weight delivering 0.5 psi (3.5 kPa)—simulating the localized pressure of an adult user seated or lying down—is applied for precisely two minutes. Shenghongda’s premium cores consistently record rewet values below 0.05 grams, whereas typical market competitors often release between 0.35 and 0.85 grams of moisture back onto the test papers. This exceptional dryness performance directly validates the superior cross-linking density of our Sumitomo SAP formulation and the moisture-trapping architecture of our virgin fluff pulp envelope.
Standing leg cuff performance is evaluated on automated hydrostatic pressure head testers in accordance with ISO 1420. The hydrophobic SMS nonwoven barriers must withstand a sustained water column pressure of greater than 220 mm H₂O before any droplet penetration occurs. Mechanical tape closures undergo 180° peel strength and dynamic shear testing on dual-column universal testing machines (ASTM D1876), ensuring closures exceed 3.8 N/25mm width even after five successive opening and repositioning cycles. Microbiological assays conducted in accordance with GB 15979 and ISO 11737 verify that total aerobic bacterial counts remain strictly below 20 CFU/g, with complete absence of Staphylococcus aureus, Pseudomonas aeruginosa, hemolytic Streptococci, and fungal contaminants.
| Product Category & Size | Standard Market Packaging (pcs / 40HQ) | Shenghongda High-Density Load (pcs / 40HQ) | Payload Increase (%) | Estimated Freight Savings per Unit |
|---|---|---|---|---|
| Adult Taped Diapers (Size L) | 72,000 pcs / 40HQ | 94,000 pcs / 40HQ | +30.5% | $0.022 - $0.028 / pc |
| Adult Pull-Up Pants (Size L) | 105,000 pcs / 40HQ | 135,000 pcs / 40HQ | +28.5% | $0.016 - $0.021 / pc |
| Hospital Underpads (60x90 cm) | 210,000 pcs / 40HQ | 275,000 pcs / 40HQ | +30.9% | $0.012 - $0.017 / pc |
| Baby Diapers (Size 4 / Maxi) | 320,000 pcs / 40HQ | 410,000 pcs / 40HQ | +28.1% | $0.008 - $0.012 / pc |
| Baby Pull-Up Training Pants | 260,000 pcs / 40HQ | 330,000 pcs / 40HQ | +26.9% | $0.010 - $0.014 / pc |
5. Packaging Thermodynamics, Ocean Freight Optimization & Landed Cost Economics
In the high-volume disposable hygiene sector, international competitiveness is determined just as decisively at the container loading dock as it is on the production floor. Absorbent articles such as adult briefs, pull-up pants, and underpads are inherently high-bulk, low-density goods; under standard packing methods, a shipping container reaches its maximum volumetric capacity (cube out) long before reaching its legal maritime gross weight limit (weigh out). When overseas freight rates fluctuate unpredictably, shipping excess air across oceans imposes an unsustainable cost penalty on importers. To deliver an unassailable commercial advantage to our global B2B clients, Shenghongda has engineered proprietary hydraulic compression packaging systems that maximize 40-foot High Cube (40HQ) container payloads without damaging structural materials or degrading subsequent fluid absorption kinetics.
The core challenge of compressing absorbent articles lies in packaging thermodynamics and polymer viscoelasticity. If a diaper core containing superabsorbent polymers and elastic strands is subjected to uncontrolled, high-impact mechanical crushing, the dry, crystalline SAP granules can fracture. Fractured polymer particles generate fine dust that migrates through the tissue wrapper, while their broken edges compromise the surface cross-linking shell, leading to severe gel blocking and core leakage upon liquid exposure. Furthermore, excessive compression can cause irreversible creep and loss of elasticity in polyurethane Lycra leg bands, resulting in loose, non-functional barrier cuffs. Shenghongda’s automated packaging machinery resolves this challenge by employing a multi-stage, gradual hydraulic pre-compression cycle. Over an eight-second duration, ambient air is evacuated from the open-cell fluff pulp matrix under controlled pressure gradients, allowing the long softwood fibers to nest compactly while the SAP granules remain intact within their cushioned fiber pockets.
The commercial ramifications of this packaging engineering are profound. A standard, uncompressed 40HQ ocean container typically accommodates between 70,000 and 75,000 adult taped diapers when packaged by conventional suppliers. Through Shenghongda’s high-density vacuum packaging technology, an identical 40HQ container accommodates between 92,000 and 96,000 units—an increase in payload density of more than 28%. When shipping on high-volume trade lanes from our primary export gateways at Xiamen Port (UN/LOCODE: CNXMN) and Quanzhou Port (UN/LOCODE: CNQZ) to major discharge hubs such as Valencia, Hamburg, Manzanillo, or Buenaventura, this volumetric optimization reduces the effective ocean freight cost per diaper by $0.018 to $0.026 USD. On an annual procurement volume of 10 million units, this single engineering innovation delivers net freight savings exceeding $200,000 USD, directly bolstering the operating margins of our overseas distribution partners.
Furthermore, Shenghongda’s global trade desk works closely with leading export credit agencies, most notably China Export & Credit Insurance Corporation (Sinosure). For established institutional healthcare importers, medical distributors, and supermarket retail chains with verified financial records, we offer flexible payment structures including Open Account (OA) 30, 60, and 90-day credit terms backed by Sinosure underwriting. This liquidity support allows our overseas partners to manage their local inventory turns and cash-flow cycles with optimal flexibility, bridging the working capital gap between maritime transit and final regional hospital invoice collection.
6. Cleanroom Environmental Controls, Microbial Governance & ISO 13485 Compliance
The manufacture of intimate medical and personal hygiene products demands an absolute, uncompromising commitment to sanitary environmental control. Because disposable diapers, incontinence pads, and surgical underpads are applied directly against fragile mucous membranes, post-operative skin, or elderly perineal tissues prone to pressure sores, the presence of even trace microbiological contamination or chemical irritants can trigger severe clinical infections. Operating in strict alignment with ISO 13485:2016 and Good Manufacturing Practice (GMP) requirements, Shenghongda has instituted pharmaceutical-grade environmental controls across its entire 8,000 square meter Quanzhou manufacturing complex.
All 16 full-servo converting lines are enclosed within a certified Class 100,000 (equivalent to ISO 9001:2015 and ISO Class 8 under ISO 14644-1) cleanroom environment. The facility features continuous positive air pressure differentials (+15 to +25 Pascals) between the manufacturing core, raw material staging zones, and outer warehouse spaces, preventing any infiltration of unconditioned outdoor dust, airborne particulates, or environmental micro-insects. Incoming air undergoes three-stage filtration—comprising primary pre-filters, secondary medium-efficiency bag filters, and terminal high-efficiency particulate air (HEPA) filters delivering an air change rate exceeding 20 cycles per hour. Automated environmental sensors continuously log temperature (maintained between 20°C and 24°C) and relative humidity (controlled between 45% and 60%), strictly preventing static electricity accumulation that could interfere with ultra-light nonwoven web handling while preventing moisture absorption by unreacted polymer raw materials.
Personnel and material entry protocols reflect the highest tier of contamination risk management. Operators must pass through automated three-stage airlocks, don anti-static lint-free jumpsuits, hairnets, and nitrile gloves, and proceed through 30-second high-velocity air showers prior to entering the manufacturing floor. Daily microbial monitoring is conducted utilizing active surface swab sampling, settle-plate sedimentation assays, and total bioburden testing in accordance with GB 15979 and European Pharmacopoeia standards. Across all production lots, our total viable aerobic microbial count is guaranteed below 20 Colony Forming Units per gram (CFU/g)—a safety factor ten times cleaner than the standard 200 CFU/g ceiling permitted by international consumer product regulations—with absolute zero detection of Staphylococcus aureus, Pseudomonas aeruginosa, hemolytic Streptococci, or coliform bacteria.
7. Strategic Sourcing Roadmap & Technical Due Diligence Checklist for Importers
For international procurement directors, healthcare tender managers, and consumer goods brand executives, successfully transitioning an adult diaper sourcing program to a primary OEM/ODM manufacturing partner requires a structured, milestone-driven technical roadmap. To eliminate costly commercial misunderstandings, ensure regulatory compliance, and guarantee on-time container delivery, Shenghongda recommends that all overseas B2B buyers execute the following multi-phase due diligence checklist prior to finalizing commercial production contracts:
- Step 1: Clinical Performance & SKU Parameter Definition
Establish exact technical specifications based on the target demographic and sales channel. Differentiate clearly between retail consumer lines (prioritizing ultra-thin silhouettes, cloth-like breathability, and aesthetic packaging) and institutional hospital/nursing home lines (prioritizing high ISO 11948-1 (Rothwell Method) Rothwell retention, heavy-duty leak cuffs, and verified low rewet values). Specify exact user waist circumference ranges, target absorption capacities, and required barrier cuff heights.
- Step 2: Regulatory Dossier & Certification Verification
Audit the prospective manufacturer’s formal compliance portfolio. For the European market, demand verified European CE MDR (EU 2017/745) technical documentation, Declaration of Conformity (DoC), and FSC (Forest Stewardship Council) Chain of Custody certificates for EUDR compliance. For the North American market, verify valid U.S. FDA Establishment Registration and 510(k) Medical Device Listings under 21 CFR 880.5270. Ensure the plant maintains accredited ISO 13485:2016 certification from an internationally recognized registrar.
- Step 3: Physical Sample Presentation Kit & Bench Testing
Never approve commercial production based solely on digital product sheets. Request customized physical sample presentation kits featuring exact target raw material compositions. Subject candidate samples to independent third-party laboratory verification for strike-through time, rewet under 0.5 psi load, hydrostatic barrier head, and mechanical side-tape peel strength. Confirm that topsheet tactile softness meets consumer sensory benchmarks.
- Step 4: Tooling Customization, Packaging Artwork & Branding Sign-Off
Finalize primary polybag and secondary master carton graphic design. Ensure all regulatory labeling, barcoding (GS1 compliant), multilingual usage instructions, and batch traceability codes match destination country consumer protection laws. Approve mechanical rotary printing plates and digital film proofs prior to full-scale packaging print runs.
- Step 5: Container Load Factor & Landed CIF Freight Optimization
Collaborate with the factory logistics team to conduct rigorous volumetric load simulations. Calculate exact 20GP versus 40HQ container load counts, verifying that high-density vacuum packaging protocols maximize piece count per container. Confirm ocean freight insurance terms, port booking schedules, and explore Sinosure trade finance options for Open Account revolving credit terms.